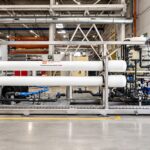
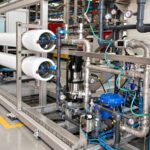
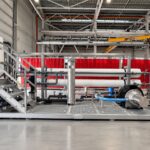
Landfill leachate is among the most challenging types of wastewater to treat due to high concentrations of organic pollutants (COD), ammonium nitrogen, dissolved salts and heavy metals, as well as significant variations in composition. Effective treatment requires carefully selected technology capable of handling demanding process conditions.
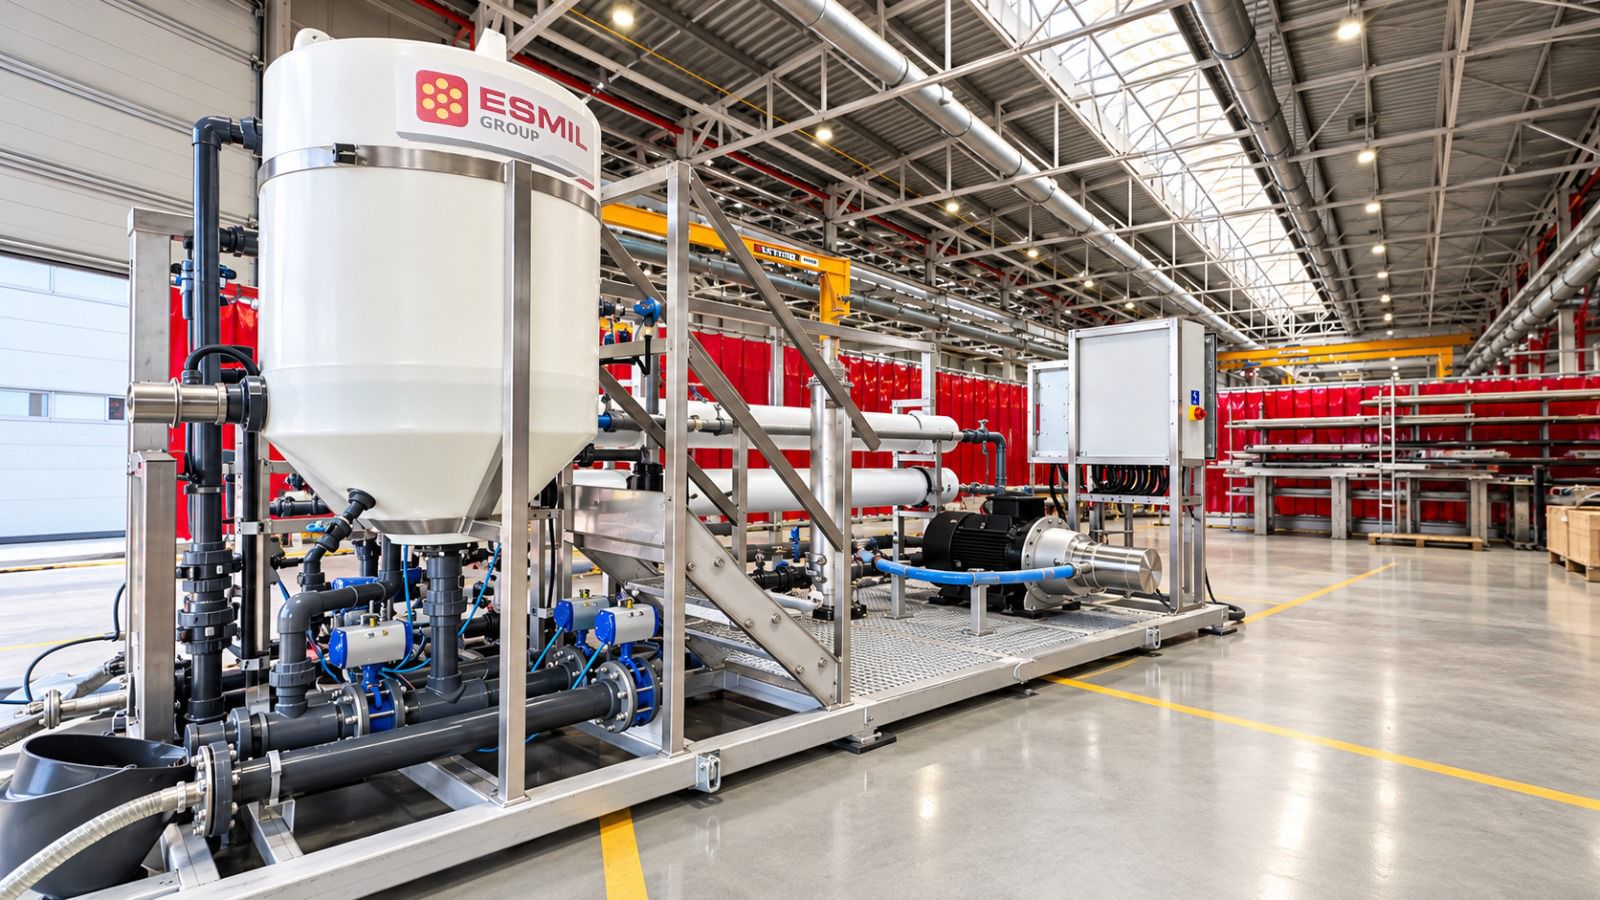
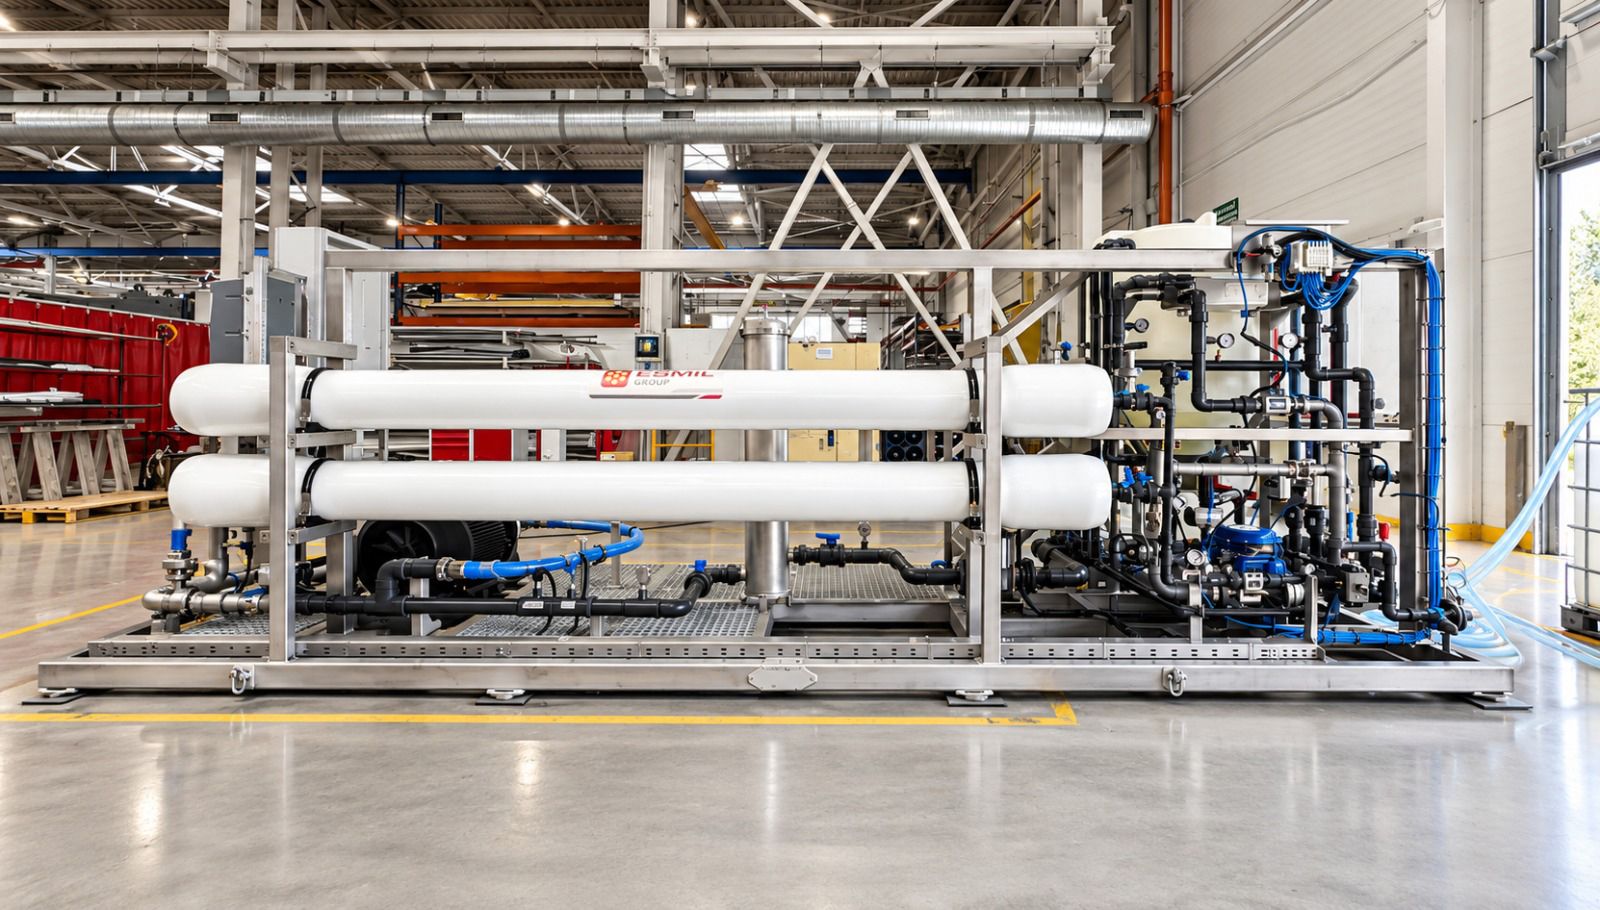
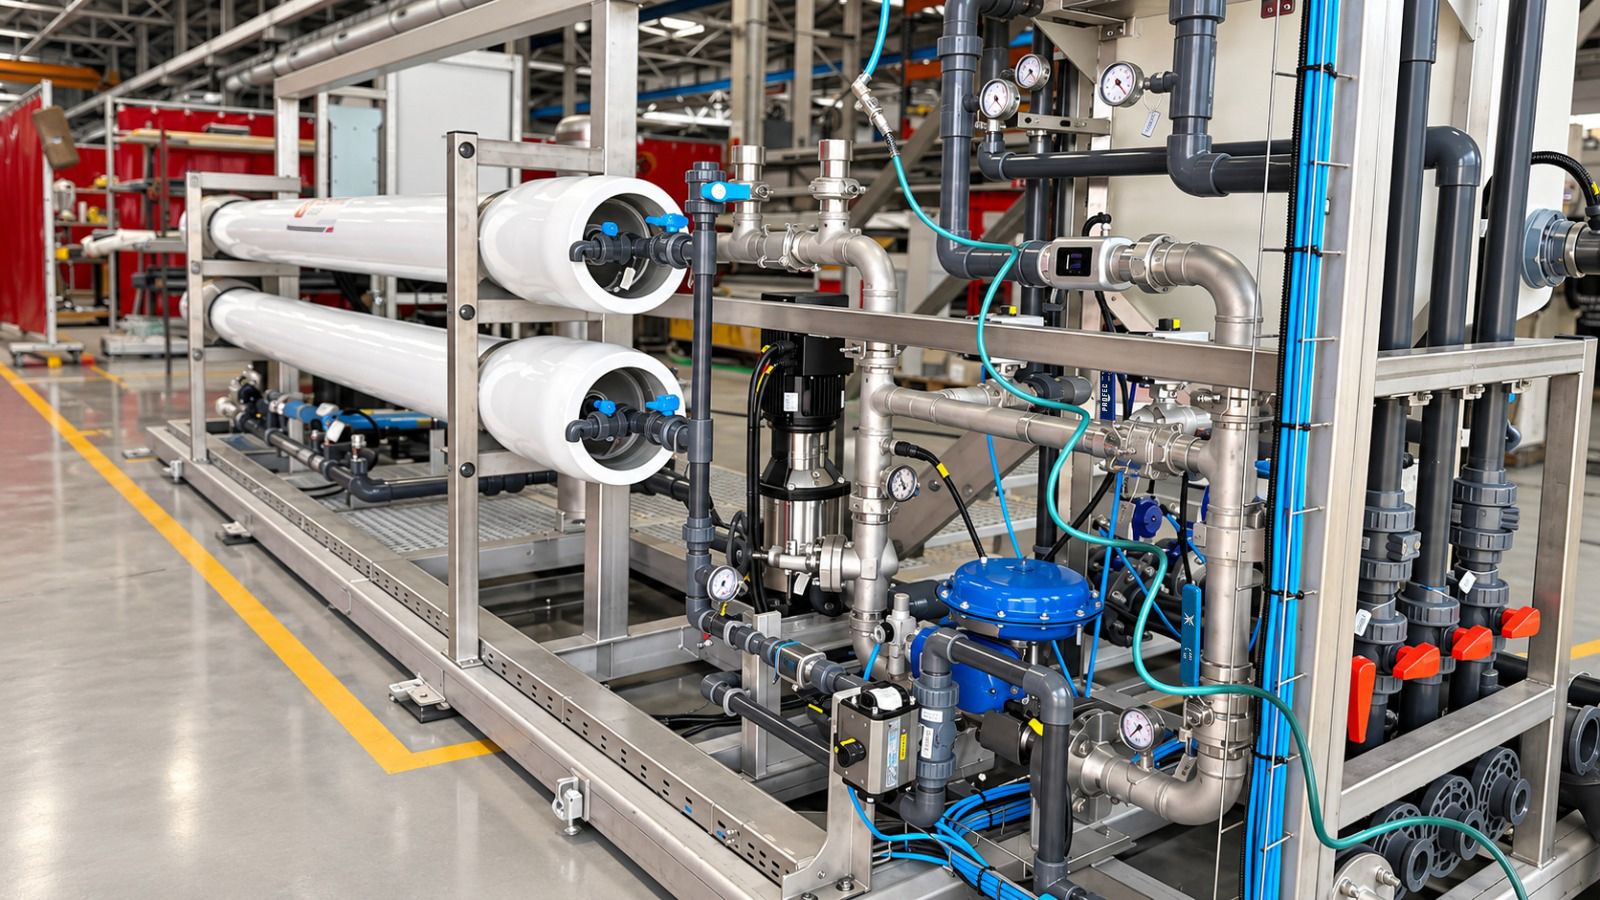
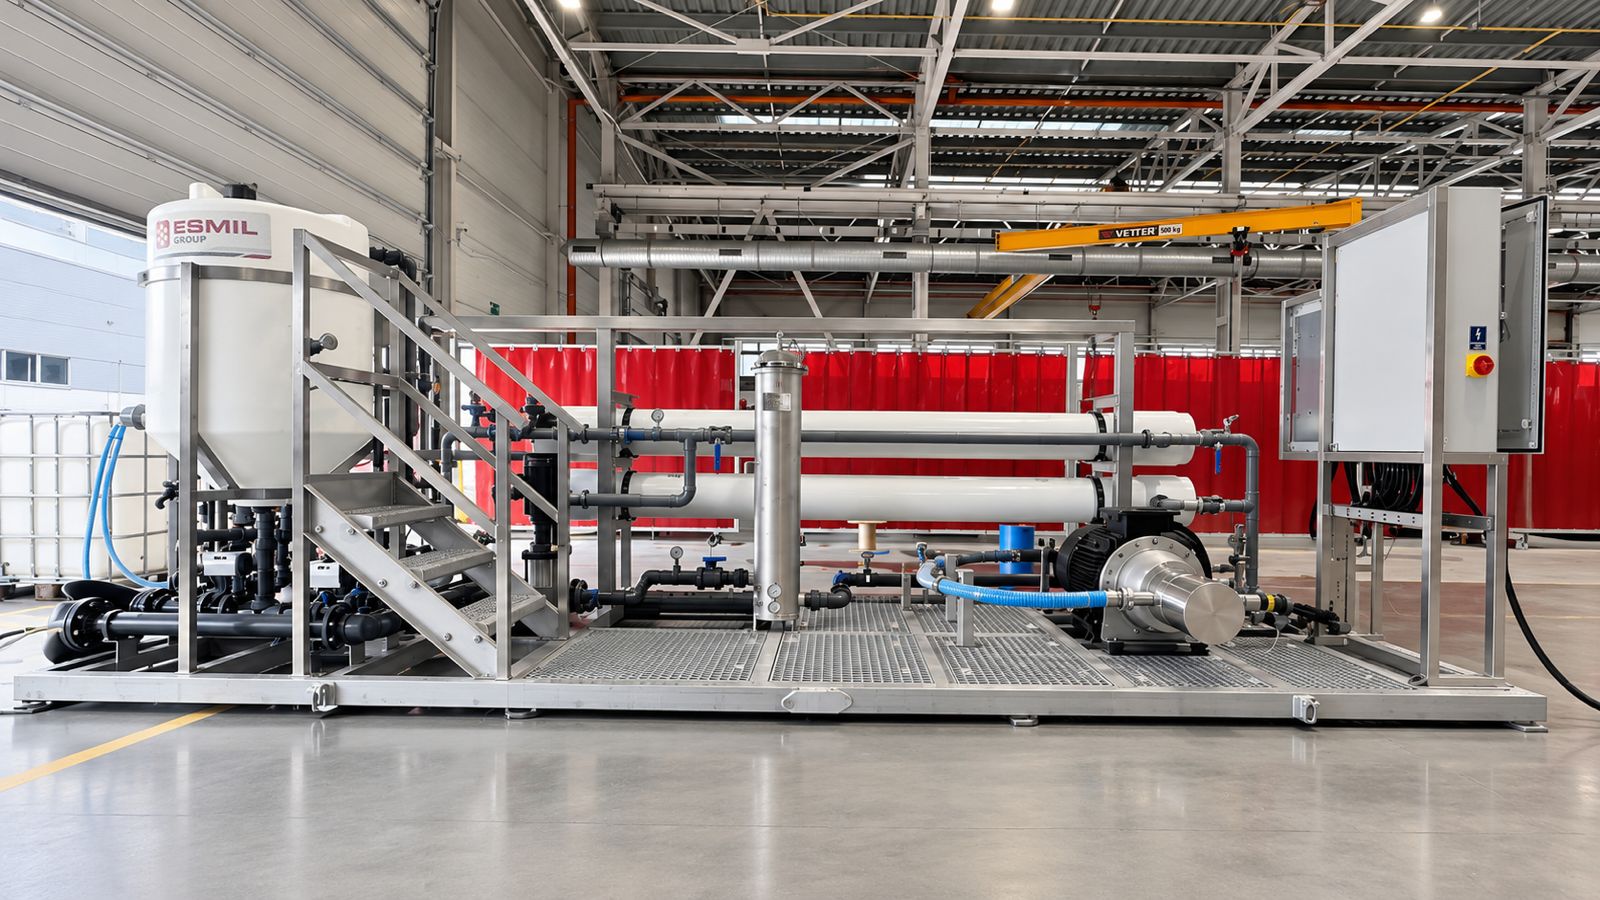
ESMIL LeachKing is a range of complete membrane treatment systems designed for a robust landfill leachate treatment and water recovery. The integrated superfiltration (SF) and reverse osmosis (RO) process provides highly effective contaminant removal, producing treated leachate that meets the required discharge standards.
Why is landfill leachate difficult to treat?
High concentrations of poorly biodegradable organic compounds, ammonium nitrogen, dissolved salts and heavy metals, combined with significant variations in leachate composition, make landfill leachate particularly challenging to treat. Under these conditions, conventional biological treatment methods may not be sufficient to meet the required discharge limits. They can also be complex and labour-intensive to operate, resulting in high operating costs and increased maintenance demands.
ESMIL LeachKing is a range of complete membrane systems designed for effective landfill leachate treatment and water recovery. Combining leachate specific superfiltration (SF) and reverse osmosis (RO) membranes, the systems deliver high contaminant removal efficiency and can achieve the treated effluent quality required for discharge, depending on feed characteristics and system configuration.
Compared to conventional biological treatment, ESMIL LeachKing offers simpler operation, lower labour requirements and a reliable treatment process that consistently delivers high-quality treated water. The membrane-based process also eliminates the generation of surplus activated sludge, reducing the need for additional sludge management.
Applications of ESMIL LeachKing Landfill Leachate Treatment System
ESMIL LeachKing systems are designed for landfill leachate sites.
With flexible process configurations, they can be used in both new leachate treatment plants and projects involving the upgrade of existing treatment systems.
Key advantages of the ESMIL LeachKing Membrane System
High treatment efficiency to meet discharge requirements
The ESMIL LeachKing Landfill Leachate Treatment System effectively removes a wide range of contaminants, including poorly biodegradable organic compounds, ammonium nitrogen, dissolved salts and heavy metals. A carefully selected system configuration ensures the required treated leachate quality, helping operators meet applicable discharge limits.
Enhanced fouling resistance and lower operating costs
ESMIL LeachKing systems use membranes with a zwitterionic surface layer that reduces organic fouling, helping maintain stable performance, extend intervals between cleaning cycles and lower chemical consumption and operating costs. A robust self-cleaning filter provides additional membrane protection by removing solid contaminants before they enter the membrane treatment stages (if needed).
High water recovery and flexible concentrate management
A design water recovery rate of 70-87% significantly reduces the volume of membrane concentrate produced. The concentrate can be recycled back to the landfill site or managed through evaporation, incineration, or solidification depending on the local regulation requirements, while treated water can be reused on-site or discharge to the local sewer, for example, for landscape irrigation. Unlike biological treatment, the membrane process does not inherently generate additional biological sludge.
Modular design
The modular design of ESMIL LeachKing treatment systems allows each configuration to be tailored to the required treatment capacity, leachate characteristics and specific project requirements. This ensures a better match between the treatment system and actual operating conditions.
Integrated control and improved process monitoring
A single central control system integrates all treatment stages, enabling continuous monitoring of key process parameters and coordinated equipment operation. This provides better oversight of the treatment process and simplifies day-to-day operation.
European manufacturing and end-to-end project delivery
ESMIL LeachKing membrane systems are designed and manufactured by ESMIL in Europe. From equipment selection and system design to integration and commissioning, a single manufacturer is responsible for project delivery, helping streamline coordination at every stage.
Reduced operating costs
Thanks to their specialized design, ESMIL membranes require significantly less frequent cleaning than conventional membranes. They can be cleaned using inexpensive, widely available acids and alkalis instead of costly specialized membrane cleaners. This reduces chemical consumption, maintenance costs, and operating expenses, contributing to a faster return on investment.
How does the ESMIL Landfill Leachate Treatment System work?
The ESMIL LeachKing system treats landfill leachate through a series of treatment stages. Depending on the leachate composition, the process may begin with DAF pretreatment. The leachate then passes through a self-cleaning filter, which removes solid contaminants before the leachate enters the membrane treatment system.
The next stage involves superfiltration (SF), followed by two-stage reverse osmosis (RO), which removes dissolved contaminants and produces treated water that meets the required quality standards.
The membrane stages also produce concentrate streams that require appropriate handling or further treatment.
The system also includes an integrated clean-in-place (CIP) system for membrane cleaning and a central control system that coordinates the individual treatment stages and enables continuous monitoring of key process parameters.
Real projects. Proven performance.
Explore real-world applications and treatment results achieved with ESMIL membrane systems.
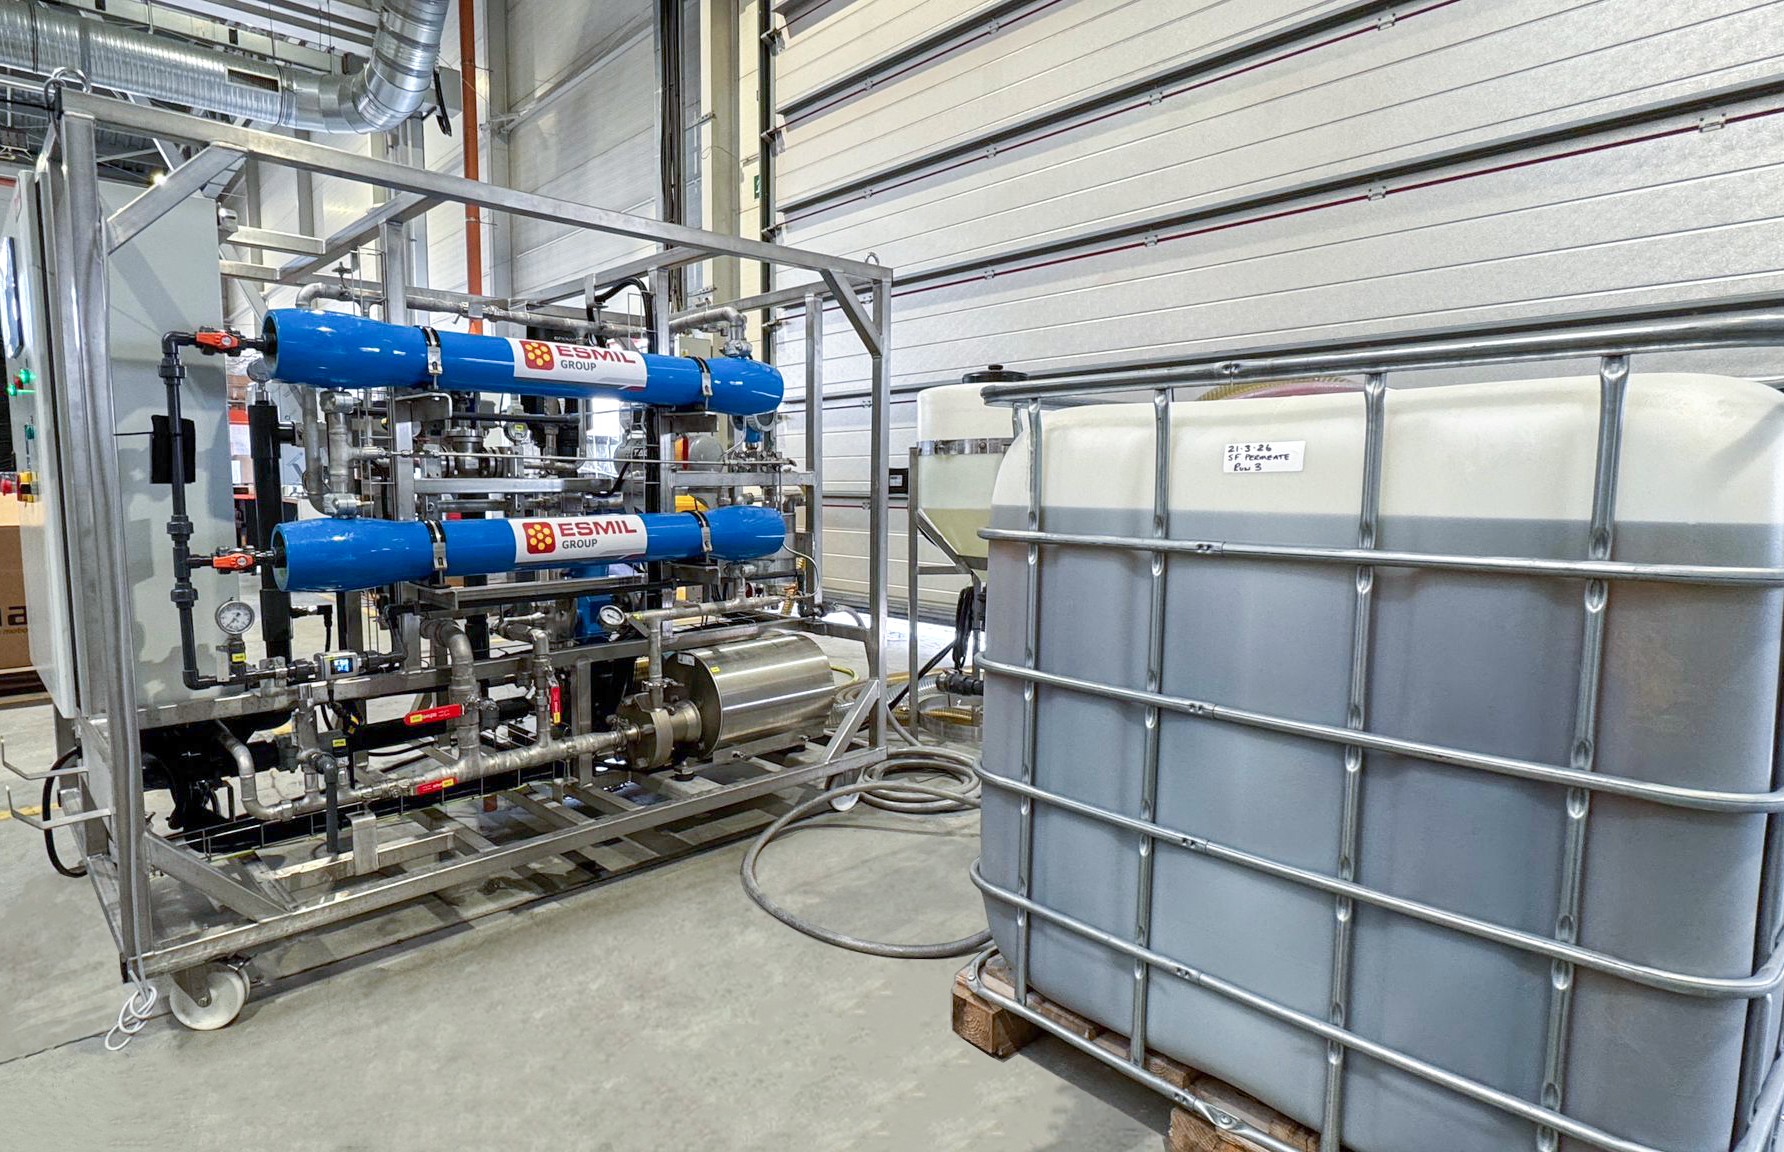
Eko-Mazury Waste Management Company, Ełk, Poland
- Challenge: Landfill leachate with extremely high COD (11,843 mg/L) and ammonium nitrogen (1,772 mg/L) concentrations
- Solution: An ESMIL treatment system combining dissolved air flotation (DAF), superfiltration (SF) using zwitterionic membranes and two-stage reverse osmosis (RO).
- Results: Over 99.8% COD reduction and over 99% ammonium nitrogen reduction, with final concentrations below 10 mg/L for both parameters.
Compare Your Current Membrane OPEX with ESMIL Performance
Enter your operating data to compare cumulative operating costs and see how long it takes for ESMIL to become the more cost-effective option.